


Rotary furnaces are the workhorses of aluminium recycling. They handle contaminated scrap, dross, and low-grade material that other furnaces cannot process economically. But they are also energy-intensive. In my 25 years, I have seen rotary furnaces consuming 900–1,200 kWh per tonne when they should be running at 600–750 kWh per tonne.
The difference is not the furnace. It is the heat transfer. Radiation, convection, and direct contact between the hot refractory and the charge all matter. When one of them is poor, the furnace runs longer, burns more gas, and loses more metal to oxidation.
Here is how to improve heat transfer efficiency in a rotary furnace, based on what I have seen work in foundries across China, Southeast Asia, India, the UK, Europe, and North America.
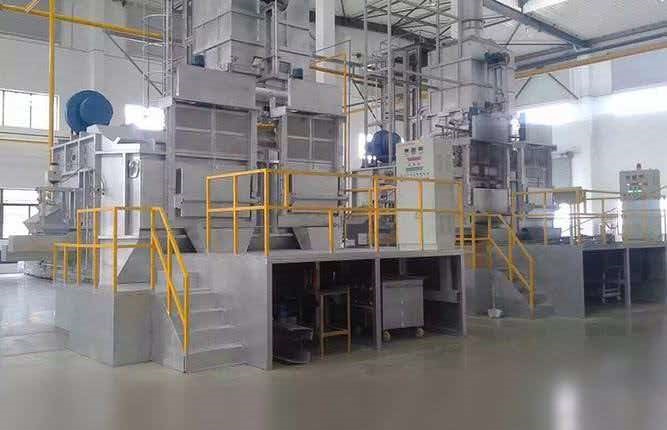
Understand the Three Heat Transfer Mechanisms
Before you change anything, understand how heat actually reaches your metal.
| Mechanism | How It Works | Share of Total Heat |
|---|---|---|
| Radiation | Flame and hot refractory radiate heat to the charge surface | 80–85% |
| Convection | Hot combustion gases circulate and transfer heat | 10–15% |
| Conduction | Hot refractory contacts the charge directly as the drum rotates | 5–10% |
Numerical simulation of an aluminium rotary furnace showed that radiation is the dominant mechanism, accounting for approximately 84% of the total heat flux received by the melting zone-1. That means most of your improvement effort should focus on radiation — and the factors that influence it.
Optimise Rotation Speed and Charging
The rotary action is what makes a rotary furnace different. As the drum turns, the refractory lining heats up, then contacts the charge directly, transferring heat by conduction. The charge tumbles, exposing fresh surfaces to radiation.
But rotation speed matters. Too slow, and the refractory does not contact the charge often enough. Too fast, and the charge is thrown against the wall without proper mixing.
Research on aluminium rotary furnaces found that a rotational speed of 1.2 rpm leads to the minimum melting time. That is a useful starting point for most furnaces. If your furnace runs slower or faster, test different speeds and measure the effect on melt time.
Charging practice also matters. The ROTANACE project, led by GHI Smart Furnaces, focused on automating furnace rotation and charging to make the process more stable and less energy-intensive. Machine learning models now predict the optimal charging times based on scrap composition and furnace state, reducing reliance on operator experience.
I have seen foundries improve melt time by 10–15% simply by charging at the right moment — not too early, not too late. The charge should be added when the lining is at its hottest, not when the furnace is cooling down between melts.
Increase Refractory Emissivity
This is the single most overlooked improvement. Refractory emissivity determines how effectively the lining radiates heat to the charge. Higher emissivity means more radiation reaches the metal.
Research showed that increasing the radiation emissivity of the refractory lining from 0.7 to 0.85 increased the radiation share of heat transfer from 84% to 88.5%, reduced exhaust gas temperature, and decreased furnace operation time by 20 minutes per cycle.
That is a significant saving. On a furnace running 20 cycles per week, that is almost seven hours of production time recovered every week.
How do you increase emissivity? Select refractory materials with higher emissivity ratings. Some high-alumina castables and silicon carbide-based refractories have naturally higher emissivity than standard firebrick. Ask your refractory supplier for emissivity data before you buy.
I have also seen foundries apply high-emissivity coatings to existing linings. The results vary, but when the coating is properly applied and maintained, emissivity improvements of 0.05–0.10 are achievable.
Optimise Burner Angle and Nozzle Parameters
The burner is your heat source. If it is aimed wrong, the heat goes to the wrong place.
Research on burner angle in aluminium rotary furnaces showed that changing the burner angle from 0° to 10° decreased furnace operation time by 35 minutes and increased thermal efficiency from 65% to 74.7%-. The higher angle improved fuel-oxygen mixing and increased the residence time of combustion gases in the furnace.
Burner nozzle diameter also matters. A study on drum rotary furnaces found that optimising nozzle parameters reduced charge melting time by 23.66% when using 25% oxygen-enriched oxidiser. With 35% enrichment, melting time fell by a further 12%.
Oxygen-enhanced combustion (OEC) is a powerful tool for rotary furnaces. A modified burner using OEC reduced total natural gas consumption by up to 60% in laboratory testing, and increased productivity by shortening melting time by up to 16%. The optimal oxygen concentration was 35% by volume — beyond that, fuel savings were marginal while NOx emissions rose rapidly.
If your furnace does not have an oxygen-enriched burner, this is worth evaluating. The payback period is often under a year.
Manage Salt Flux for Better Heat Transfer
Salt flux is essential in rotary furnaces. It protects the molten metal from oxidation and collects oxides from the scrap-. But the amount of salt affects heat transfer and metal recovery.
A study on fluxing in aluminium refining found that metal recovery increases with salt content in both rotary and crucible furnaces. For tilting rotary furnaces, the salt factor can be as low as 0.4 to 0.8, compared to 0.9 to 2.0 for fixed-axis rotary furnaces-. Lower salt factor means less salt consumption, lower cost, and less waste.
The mechanism is simple. The salt flux covers the molten metal and captures oxides. When the furnace rotates, the hot refractory contacts the salt-metal mixture directly, transferring heat by conduction-. If the salt layer is too thick, it insulates the metal from the refractory. If it is too thin, oxidation increases and metal recovery falls.
I recommend measuring your salt factor and adjusting it based on scrap quality. For clean, low-oxide scrap, a lower salt factor works. For heavily contaminated scrap, you need more salt — but you also need to check that the furnace rotation is mixing the charge properly.
Preheat Scrap and Combustion Air
Waste heat recovery is one of the most cost-effective improvements for any furnace. In a rotary furnace, the exhaust gases leave at high temperature. That heat can preheat incoming scrap or combustion air.
One study found that the exhaust from a typical aluminium melting furnace contains enough waste heat to preheat scrap to 482–538°C and simultaneously preheat combustion air to 427–482°C. The energy savings from this alone can be substantial.
Scrap preheating also reduces the moisture content, which is critical. Wet scrap causes steam explosions, thermal shock, and hydrogen pickup. Preheating drives off moisture before the scrap enters the melt.
I have written about how to optimise burner efficiency before, and the principles apply here too. Measure your flue gas temperature. If it is above 400°C after the recuperator, you are losing heat that could be recovered.
Reduce Heat Loss Through the Shell
A rotary furnace shell radiates heat to the environment. The thicker and better-insulated the lining, the less heat escapes. But many foundries use thin linings to increase furnace volume, trading insulation for capacity.
That is usually a mistake. A lightweight back-up refractory system, developed specifically for aluminium rotary furnaces, improves thermal efficiency of the installed lining without sacrificing capacity-. The key is the multi-layer design: a dense hot-face layer for wear resistance and a lightweight insulating layer for thermal efficiency.
Check your shell temperature with a thermal camera. If the shell is above 120°C, you are losing heat. If it is above 150°C, you are losing a lot. The cost of a better lining system pays back in reduced gas consumption within months.
A Real Case from Southeast Asia
In 2023, a recycling plant in Malaysia was running two rotary furnaces. Energy consumption was 980 kWh per tonne. Melt time was 4.5 hours per cycle. Metal recovery was 82%.
We made four changes:
Increased burner angle from 0° to 8°.
Switched to a high-emissivity refractory for the hot-face layer.
Implemented automated charging based on lining temperature.
Installed a scrap preheating system using waste heat.
Results after one month:
- Energy consumption: 980 → 784 kWh/t (20% reduction)
- Melt time: 4.5 → 3.6 hours (20% faster)
- Metal recovery: 82% → 89% (7% improvement)
- Annual savings: over $210,000
The investment was $42,000. Payback was under three months.
A Simple Improvement Checklist
Measure your current energy consumption per tonne. If you do not measure it, you cannot improve it.
Check burner angle. A 5–10° change can improve thermal efficiency by 10%.
Test different rotation speeds. Start at 1.2 rpm and adjust based on melt time.
Ask your refractory supplier for emissivity data. Higher is better.
Measure salt factor. Lower it for cleaner scrap.
Check shell temperature with a thermal camera. If it is above 120°C, improve insulation.
Evaluate scrap preheating. Waste heat is free.
Consider oxygen enrichment if your furnace does not have it.
Track melt time and gas consumption weekly.
Train operators on the relationship between charging practice and heat transfer.
Final Thoughts
Improving heat transfer in a rotary furnace is not about buying a new furnace. It is about optimising the one you have. Radiation is the dominant mechanism. Rotation speed, refractory emissivity, burner angle, and salt flux management all influence it.
In my 25 years, I have seen foundries cut energy consumption by 15–25% without major capital investment. They measured, adjusted, and monitored. The improvements compounded over time.
If you run a rotary furnace, start with the burner angle. Then check your refractory emissivity. Then look at rotation speed and charging practice. You will see the difference in your first month.
Internal links: How to Optimize Burner Efficiency in Gas-Fired Aluminium Furnaces, How to Reduce Oxidation Loss in Aluminium Melting Operations, Furnace Maintenance Checklist
About the Author: Hu Shenyue is a veteran aluminium melting furnace expert with 25 years of hands-on experience in China, Southeast Asia, India, the UK, and Europe. He writes practical, experience-based content on furnace selection, maintenance, and optimisation at SmeltPro.
