How a Chinese expert helped an aerospace foundry achieve AMS 2770 compliance. Heat treatment, TUS, SAT, quench delay, records, and training.
In early 2024, I received a call from a quality director at an aerospace foundry in Jiangsu Province. His company produces aluminium alloy castings for commercial aircraft and defence programmes. They had been supplying non-critical parts for years. Now, a European Tier 1 supplier wanted them to produce flight-critical castings. The condition was simple: they needed AMS 2770 compliance.
The foundry had failed its first AMS 2770 audit six months earlier. The auditors issued four major non-conformances. The quality director told me: “We thought our heat treatment was fine. We were wrong. We do not understand what AMS 2770 actually requires.”
I spent two weeks on site. Six months later, the foundry passed the AMS 2770 audit with zero major non-conformances. This is how we did it.
What Is AMS 2770 and Why Does It Matter
AMS 2770 is the SAE Aerospace Material Specification for heat treatment of aluminium alloy castings. It covers the thermal processing required to achieve specified mechanical properties in castings — solution heat treatment, quenching, and precipitation ageing.
It is not optional for aerospace work. If you supply flight-critical aluminium castings, your customer will require AMS 2770 compliance. The standard references AMS 2750 for pyrometry requirements, including furnace classification, Temperature Uniformity Surveys (TUS), and System Accuracy Tests (SAT).
The audit is not a management system review. It is a technical audit. The auditors examine your equipment, your procedures, your records, and your people. They focus on specific process parameters, not on whether your quality manual is well written.
The Starting Point: Four Major Non-Conformances
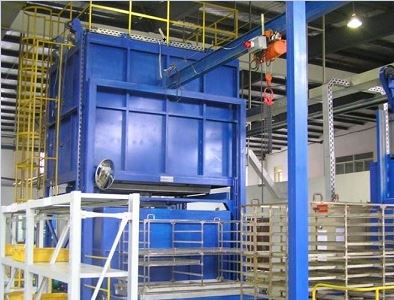
The Jiangsu foundry operates a gas-fired solution heat treatment furnace and an ageing furnace. They cast A356 and A357 alloys for structural components. Production is around 2 tonnes per day, two shifts, five days per week.
The first audit failed on four major points:
| Non-Conformance | Details | Root Cause |
|---|---|---|
| Furnace temperature uniformity | TUS showed ±18°C deviation | No formal TUS schedule |
| Quench delay time | 28 seconds from furnace to quench | Manual transfer, no procedure |
| System Accuracy Test (SAT) | Not performed per AMS 2750 | No SAT procedure or records |
| Process records | Only 5 consecutive batch records available | No systematic retention |
There were also minor findings: quench water temperature not controlled, ageing furnace calibration missing, and personnel training not documented.
The pattern was clear. The foundry had good equipment and competent people. But they did not understand what AMS 2770 actually requires. They thought AS9100 was enough. It is not.
Step 1: Understanding AMS 2770 and AMS 2750
The first thing I did was explain the relationship between AMS 2770 and AMS 2750.
AMS 2770 tells you what heat treatment process to use for aluminium castings. AMS 2750 tells you how to measure and control temperature. If you do not understand AMS 2750, you cannot comply with AMS 2770.
The key concepts are:
Furnace classification — based on temperature uniformity across the working zone
Temperature Uniformity Survey (TUS) — verifies furnace uniformity
System Accuracy Test (SAT) — verifies the entire measurement system
Instrumentation type — defines calibration requirements
Quench delay — time from furnace door opening to complete immersion
For aluminium castings, the critical parameters are solution temperature, quench delay, quench water temperature, and ageing temperature.
Step 2: Perform a Temperature Uniformity Survey (TUS)
A TUS is a mandatory requirement for all thermal processing equipment used in aerospace under AMS 2750. The TUS verifies the furnace’s temperature uniformity across the qualified working zone.
We conducted a full TUS with a calibrated data logger and multiple thermocouples positioned throughout the working zone. The results:
| Location | Temperature Deviation |
|---|---|
| Front left | +9.2°C |
| Front right | -8.6°C |
| Centre | +1.4°C |
| Back left | -12.8°C |
| Back right | +10.4°C |
The maximum deviation was -12.8°C. The aerospace requirement for aluminium solution treatment is typically ±6°C or better, depending on the alloy and specification. The furnace was out of tolerance.
We made three changes:
Repositioned the thermocouples. The original control thermocouple was in one corner. We added a second thermocouple near the door. The controller now averages the two readings.
Improved circulation. The furnace had poor air circulation. We adjusted the burner angle and added a baffle to direct hot gases more evenly.
Re-tuned the PID. The controller was set for a larger furnace. We re-tuned it for the actual volume and heat transfer characteristics.
After the changes, the maximum deviation dropped to -3.8°C. The furnace now qualified within tolerance.
I have written about how to fix a furnace that is not reaching setpoint temperature. The principles apply to TUS preparation.
Step 3: Implement System Accuracy Tests (SAT)
A SAT verifies the accuracy of the entire measurement system — thermocouple, extension wire, controller, and recorder. The aerospace requirement is that SAT error must be within ±1.1°C.
We implemented a formal SAT procedure:
A calibrated reference thermocouple was placed adjacent to the furnace control thermocouple.
Both readings were recorded at three temperatures: 500°C, 540°C, and 580°C.
The difference between the control reading and the reference reading was calculated.
The first SAT revealed a problem. The control thermocouple was reading 2.4°C high. That was outside the ±1.1°C tolerance. We replaced the thermocouple and re-ran the test. The error dropped to 0.5°C.
We established a SAT schedule:
| Activity | Frequency |
|---|---|
| SAT | Quarterly |
| Thermocouple calibration | Every 6 months |
| Controller calibration | Annually |
| TUS | Quarterly (for Class 2, Type B) |
The TUS frequency was determined by the furnace class and instrumentation type. For a Class 2 furnace with Type B instrumentation, the initial TUS interval is monthly until four consecutive successful surveys, then quarterly.
Step 4: Fix the Quench Delay
Quench delay is the time from when the furnace door opens to when the casting is fully immersed in the quench tank. For aluminium castings, AMS 2770 requires a maximum delay of 15 seconds. The foundry was at 28 seconds.
We made four changes:
Installed a faster transfer mechanism. The original manual transfer was slow. We installed a pneumatic transfer arm that moves the load from furnace to quench in 6 seconds.
Modified the furnace door. The original door was slow to open. We installed a counterbalanced door that opens in 3 seconds.
Repositioned the quench tank. The tank was 4 metres from the furnace. We moved it to 1.5 metres.
Trained operators. They practised the transfer until they could consistently achieve under 12 seconds.
Cost: $18,000 for the transfer mechanism and modifications.
The result: quench delay dropped to 9 seconds. That was within the 15-second limit with margin.
Step 5: Control Quench Water Temperature
The quench water temperature was not controlled. It varied from 25°C in winter to 45°C in summer. AMS 2770 requires quench water temperature to be controlled within a specified range — typically 60–82°C for hot water quenching of aluminium castings.
We installed a simple water heater and circulation system. The cost was $6,500. The temperature is now maintained at 70°C ±3°C.
We also installed a temperature recorder. The operator logs the quench water temperature before every load. The data is retained for audits.
Step 6: Upgrade the Ageing Furnace
The ageing furnace was also out of compliance. The TUS showed deviations of ±10°C. The ageing temperature for A356 is typically 155–170°C, with a tolerance of ±6°C.
We performed a TUS on the ageing furnace and found similar circulation problems. We adjusted the fan and repositioned the thermocouple. The deviation dropped to ±3°C.
We also calibrated the ageing furnace controller and established a SAT schedule.
Step 7: Establish Process Records and Traceability
AMS 2770 requires documented evidence of process control. The aerospace standard requires at least 20 consecutive batch records of process data. The foundry had only 5.
We implemented a process recording system:
| Data Point | Recording Method | Retention Period |
|---|---|---|
| Solution temperature | Continuous chart recorder | 10 years |
| Quench delay time | Manual log with time stamp | 10 years |
| Quench water temperature | Manual log with time stamp | 10 years |
| Ageing temperature | Continuous chart recorder | 10 years |
| SAT results | Calibration log | 10 years |
| TUS results | Survey report | 10 years |
| Charge material | Barcode scanning | 10 years |
| Melt chemistry | Spectrometer report | 10 years |
Every load was assigned a unique heat treatment number. The number linked to all process data. The data became part of the traceability record that AMS 2770 auditors would review.
Step 8: Personnel Training and Qualification
AMS 2770 requires that heat treatment personnel be trained and qualified. The aerospace standard requires operators to complete recognised training.
We developed a training programme:
- Pyrometry fundamentals — thermocouple types, calibration, accuracy
- AMS 2750 requirements — furnace classification, TUS, SAT
- AMS 2770 requirements — solution treatment, quenching, ageing
- Process control — temperature recording, quench delay, alarm response
- Documentation — how to complete records accurately
We also sent two senior engineers to a PRI-approved pyrometry training course. They became the plant’s internal pyrometry experts.
The training was documented. Each operator signed a training record. The records were filed with the audit documentation.
Step 9: Write the AMS 2770 Procedure
AMS 2770 requires a written heat treatment procedure that covers all aspects of the standard. The plant had none.
We wrote a 12-page procedure covering:
- Solution treatment temperature and time
- Quench delay requirements
- Quench water temperature and agitation
- Ageing temperature and time
- Furnace classification and working zone
- Thermocouple types and calibration requirements
- Instrumentation accuracy requirements
- SAT procedure and frequency
- TUS procedure and frequency
- Record retention requirements
- Corrective action for out-of-tolerance conditions
The procedure was written in plain language. It was not a 100-page manual that nobody would read. It was a working document that operators could follow.
Step 10: Prepare for the Audit
Six months after the first failed audit, we conducted a pre-audit gap analysis. We used the AMS 2770 audit checklist as our guide. We checked every item:
- Was the heat treatment procedure written?
- Were TUS and SAT records complete?
- Were thermocouple calibrations current?
- Were operators trained and documented?
- Were process records retained for at least 20 batches?
- Was the furnace classified?
- Was quench delay within 15 seconds?
- Was quench water temperature controlled?
We found three minor gaps. We closed them within two weeks.
The Audit Results
The AMS 2770 audit was conducted over three days. The auditor reviewed documentation, observed the furnace in operation, and interviewed operators.
The result: zero major non-conformances. Three minor observations.
| Audit Area | Result |
|---|---|
| Heat treatment procedure | Compliant |
| TUS records | Compliant |
| SAT records | Compliant |
| Thermocouple calibration | Compliant |
| Quench delay | Compliant (9 seconds) |
| Quench water temperature | Compliant (70°C ±3°C) |
| Ageing furnace | Compliant |
| Process records | Compliant (20+ batches) |
| Personnel training | Compliant |
| Furnace classification | Compliant |
The foundry received AMS 2770 compliance. They can now bid on flight-critical aerospace work.
The Results After Six Months
| Metric | Before | After | Improvement |
|---|---|---|---|
| TUS deviation | ±18°C | ±3.8°C | 79% reduction |
| Quench delay | 28 seconds | 9 seconds | 68% reduction |
| SAT error | 2.4°C | 0.5°C | 79% reduction |
| Process records | 5 batches | 20+ batches | 4x more |
| Audit result | Failed | Passed | — |
| Aerospace contract value | — | $3.2 million/year | — |
| Investment | — | $32,000 | Payback: <2 months |
The quality director called me six months later. He said: “We just passed our second surveillance audit with zero findings. The system is working.”
What Made the Difference
Three things drove the improvement:
1. Understanding AMS 2750. The plant had good equipment. They did not understand the standard. Once they understood furnace classification, TUS, and SAT, the path forward was clear.
2. Systematic record-keeping. AMS 2770 is not just about doing the right thing. It is about proving you did the right thing. Records are the proof.
3. Training. The auditors interview operators. If operators cannot explain what they do and why, the audit fails. Training made the difference.
What You Can Apply
If you are preparing for AMS 2770 compliance, ask yourself these questions:
Is your furnace classified per AMS 2750? If not, perform a TUS.
Are your SAT records current and complete? If not, implement a SAT schedule.
Is your quench delay under 15 seconds? If not, improve your transfer system.
Is your quench water temperature controlled? If not, install a heater and circulation system.
Do you have a written heat treatment procedure? If not, write one.
Are your process records retained for at least 20 consecutive batches? If not, start recording.
Are your operators trained and documented? If not, train them.
Do you have a corrective action system that closes findings? If not, build one.
These are not theoretical. They are the minimum requirements for AMS 2770 compliance. I have seen foundries in China, Southeast Asia, and Europe fail because they ignored one of these.
When to Call an Expert
You can prepare for AMS 2770 yourself. But the standard is complex and the audit is strict. The Jiangsu foundry had competent engineers. They had AS9100 certification. But they did not understand AMS 2750.
My fee for the two-week audit and preparation support was $18,000. The value of the aerospace contract was over $3.2 million per year. That is a good return.
If you are preparing for AMS 2770, bring in a specialist early. The cost of a consultant is small compared to the cost of a failed audit.
Final Thoughts
AMS 2770 compliance is not about buying a new furnace. It is about controlling temperature, quench delay, quench water, and documentation. Each one must be right. If one fails, the others cannot compensate.
In my 25 years, I have seen China move from importing almost everything to producing over half the aluminium in its own commercial aircraft. That is not a small achievement. But the gap between what China can do and what it needs to do remains the defining challenge of the next decade.
For foundries entering aerospace work, the message is simple: this is a different game. It demands different furnaces, different processes, and different standards. The ones who understand this will win. The ones who do not will be left behind.
Internal links: How to Achieve Aerospace-Grade Aluminium Melt Cleanliness, Case Study – Achieving NADCAP Certification for a Sichuan Aerospace Melting Plant, Case Study – How a Chinese Expert Achieved Aerospace Melt Purity for a US Supplier, The State of China’s Aerospace Aluminium Melting Industry – Expert Analysis, How to Fix a Furnace That Is Not Reaching Setpoint Temperature.