High melt loss is the silent killer of profitability in aluminium recycling. You charge 100 tonnes of scrap. You pour 85 tonnes of metal. Where did the other 15 tonnes go? It went to dross, salt slag, oxidation, and dust. Every kilogram of that lost metal was paid for. Every kilogram is a loss.
I have spent 25 years troubleshooting aluminium scrap melting furnaces in China, Southeast Asia, India, Europe, and North America. High melt loss is one of the most common problems I see. And it is almost always fixable without buying new equipment.
In 2023, I worked with a recycling plant in Binh Duong, Vietnam. They were melting 25 tonnes per day of mixed scrap. Their melt loss was 12.8%. That meant 3.2 tonnes of metal lost every day. At $2,500 per tonne, that was $8,000 per day. Over a year, it was $2.9 million.
I spent five days on site. By the end of the following month, melt loss had dropped to 7.4%. The annual saving was over $1.6 million.
This is how we did it.
The Starting Point: 12.8% Melt Loss
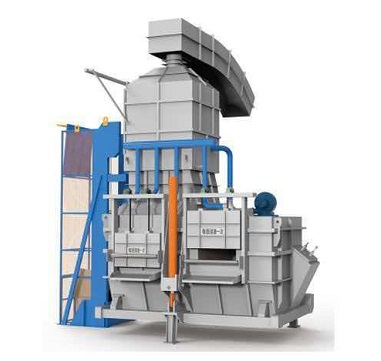
The plant operates a 5-tonne tilting rotary furnace feeding an ingot casting line. They melt around 25 tonnes per day of mixed scrap — UBC, extrusion offcuts, turnings, and post-consumer material. The plant runs two shifts per day, six days per week.
The problems were visible from the first day:
| Issue | Measurement | Impact |
|---|---|---|
| Melt temperature | 780°C | Excessive oxidation |
| Skimming frequency | Every 20 minutes | Metal lost with each skim |
| Dross metal content | 46% | High metal loss in dross |
| Salt factor | 1.2 | High salt consumption, high slag volume |
| Scrap storage | Outdoors, uncovered | Wet scrap, moisture pickup |
| Burner flue oxygen | 7.8% | Excess air, heat loss |
| Recuperator condition | Blocked | No heat recovery |
The plant manager admitted they had no formal measurement system. They relied on the furnace controller display. They had never used a hydrogen analyser. The operators had never been trained on the relationship between furnace parameters and melt loss.
I told him: “Your furnace is not the problem. The system is the problem. We need to measure everything before we change anything.”
Step 1: Measure Where the Metal Goes
You cannot fix what you cannot measure. The first step is to set up a simple measurement system.
| Data Point | How to Measure | Frequency |
|---|---|---|
| Metal charged | Weighbridge or load cell | Every charge |
| Metal poured | Weighbridge or load cell | Every cast |
| Dross weight | Scale | Every skim |
| Dross metal content | Visual estimate or lab test | Daily |
| Salt slag weight | Scale | Every tap |
| Energy consumption | Gas meter or electricity meter | Daily |
Once you have this data, you can calculate melt loss per tonne. You can see which shifts are better. You can see which scrap types lose more metal. You can see the effect of a process change.
At the Vietnamese plant, the melt loss was 12.8%. That was the starting point.
Step 2: Lower Melt Temperature
Every 10°C above the minimum required melting temperature increases oxidation loss by 5–10%. I have seen plants run at 780°C because “it melts faster.” Yes, it melts faster. It also oxidises faster.
For ADC12, the recommended melt temperature is 700–730°C. For pure aluminium, 680–700°C is sufficient.
At the Vietnamese plant, the furnace was set to 780°C. We lowered it to 720°C. The operators were sceptical. They thought melt time would increase.
It did not. Because we also tuned the burner. The burner was running with 7.8% oxygen. We adjusted it to 3.2%. The flame became shorter and more intense. Melt time actually decreased by 8 minutes per cycle.
The lower temperature reduced oxidation loss immediately. The dross metal content began to fall.
The fix: Set the furnace to the lowest temperature that achieves the required melt rate. Measure the actual metal temperature, not just the controller display.
Step 3: Change Skimming Practice
Skimming is necessary. But excessive skimming removes metal along with oxide. The key is to skim less often and more gently.
At the Vietnamese plant, operators were skimming every 20 minutes. The dross metal content was 46%. They were throwing away metal with every skim.
We changed the skimming frequency to every 45 minutes. We switched to a perforated skimming tool that drains metal back into the furnace. We installed a dross press to recover residual metal from the dross.
Cost: $12,000 for the dross press and tools.
The result: dross metal content dropped from 46% to 26%. Metal recovery improved by 3.5%.
I have written about how to improve metal recovery in aluminium scrap melting. Skimming practice is one of the key factors.
Step 4: Optimise Salt Flux
Salt flux is essential in rotary furnaces. It protects the metal from oxidation and helps coalesce fine droplets. But too much salt increases slag volume and cost. Too little salt reduces recovery.
At the Vietnamese plant, the salt factor was 1.2. For a tilting rotary furnace, the salt factor should be 0.4–0.8.
We reduced the salt factor to 0.7. We also changed the flux composition:
| Component | Before | After |
|---|---|---|
| NaCl | 50% | 40% |
| KCl | 45% | 35% |
| Cryolite (Na₃AlF₆) | 5% | 25% |
The higher cryolite content helps strip oxides from the metal surface and reduces slag viscosity. Metal recovery improved by 2 percentage points.
The fix: Match salt factor to scrap type. Use higher cryolite content for better oxide removal.
Step 5: Control the Furnace Atmosphere
The atmosphere inside your furnace matters. If it is rich in oxygen or moisture, oxidation increases.
At the Vietnamese plant, the burner was running at 7.8% oxygen. That is too high. We tuned it to 3.2%. We also checked the furnace door seals. They were worn flat. We replaced them.
We also checked for air leaks. The furnace had several small gaps around the door and burner port. We sealed them with high-temperature ceramic fibre.
Cost: $1,200 for seals and sealing material.
The result: oxygen inside the furnace dropped from 7.8% to 3.2%. Oxidation loss reduced by another 2%.
I have written about how to optimise burner efficiency in gas-fired aluminium furnaces. The principles apply here.
Step 6: Pre-Dry Scrap
Wet scrap causes steam explosions, thermal shock, and hydrogen pickup. It also absorbs heat, increasing energy consumption.
At the Vietnamese plant, scrap was stored outdoors and charged wet after rain. We built a covered drying rack and installed a simple scrap preheater using waste heat from the furnace exhaust. The preheater raises scrap temperature to 200–250°C, driving off moisture.
Cost: $2,000 for the drying rack and preheater.
The result: no more wet charging. Hydrogen pickup reduced. Melt loss reduced by another 1.5%.
Step 7: Train Operators and Measure Everything
The best equipment in the world fails without trained operators. We trained the Vietnamese team on:
-
Target melt temperature: 720°C
-
Skimming frequency: every 45 minutes
-
Salt factor: 0.7
-
Scrap must be dry before charging
-
Burner oxygen: 3.2%
We also started measuring melt loss every shift. The operators now see the results of their work. When recovery goes up, they know why. When it goes down, they know what to check.
Cost: $2,500 for training and measurement system.
The Results After One Month
| Metric | Before | After | Improvement |
|---|---|---|---|
| Melt loss | 12.8% | 7.4% | 5.4% reduction |
| Dross metal content | 46% | 26% | 20% reduction |
| Salt factor | 1.2 | 0.7 | 42% reduction |
| Melt temperature | 780°C | 720°C | 60°C lower |
| Energy consumption | 910 kWh/t | 756 kWh/t | 17% reduction |
| Annual metal savings | — | $1,460,000 | — |
| Annual energy savings | — | $186,000 | — |
| Total annual savings | — | $1,646,000 | — |
| Investment | — | $17,700 | Payback: <1 week |
The plant manager was stunned. He had been ready to buy a new furnace. He didn’t need one. He needed to fix the process.
What Made the Difference
Three things drove the improvement:
1. Lower melt temperature. Reducing from 780°C to 720°C cut oxidation loss immediately. This was the single biggest win.
2. Better skimming practice. Skimming less often and using a dross press recovered metal that was previously thrown away.
3. Lower salt factor. Reducing salt consumption from 1.2 to 0.7 reduced slag volume and metal entrapment.
I have written about how to reduce metal loss in secondary aluminium melting for ingot production. The principles are the same.
A Simple Checklist for High Melt Loss
-
Measure melt loss every shift. You cannot improve what you do not measure.
-
Set melt temperature to the minimum required. Do not run hot.
-
Skim less often — every 45 minutes, not every 20.
-
Use a perforated skimming tool. Install a dross press.
-
Match salt factor to scrap type. 0.4–0.8 for tilting rotary furnaces.
-
Use higher cryolite content in flux. 20–25% for better oxide removal.
-
Tune the burner. Target O₂ 2–4% in flue gas.
-
Check door seals. Replace when worn.
-
Pre-dry scrap. Build a covered drying rack.
-
Train operators on the metal balance.
When to Call an Expert
You can measure these things yourself. A pyrometer, a scale, and a stopwatch will tell you most of what you need to know. But sometimes an experienced eye sees the system, not just the components.
The Vietnamese plant had a competent maintenance team. They had kept the furnace running for years. But they had never been trained on metal balance or dross processing. They did not know what they did not know.
My fee for the five-day audit and commissioning support was $11,000. The annual saving was $1.65 million. That is a 150x return.
If your melt loss is above 8%, call someone. Or use the checklists on this blog. Either way, do not wait.
Final Thoughts
High melt loss in aluminium scrap melting furnaces is not inevitable. It is a signal that something in your process is out of control. Temperature, skimming practice, salt flux, atmosphere, and scrap moisture all matter.
In my 25 years, I have seen plants reduce melt loss from 15% to 5% by fixing the process, not the equipment. The furnace did not change. The people did.
If you run a recycling plant, start by measuring your melt loss and dross metal content. If either is out of specification, fix it. You will see the difference in your profit.
About the Author: Hu Shenyue is a veteran aluminium melting furnace expert with 25 years of hands-on experience in China, Southeast Asia, India, the UK, Europe, and North America. He writes practical, experience-based content on furnace selection, maintenance, and optimisation at SmeltPro.
Internal links: How to Improve Metal Recovery in Aluminium Scrap Melting, How to Reduce Metal Loss in Secondary Aluminium Melting for Ingot Production, How to Optimize Aluminium Scrap Melting Furnace Charging for Different Scrap Types, How to Optimize Burner Efficiency in Gas-Fired Aluminium Furnaces, How to Choose a Secondary Aluminium Melting Furnace for Ingot Production.